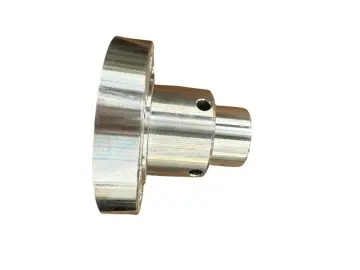
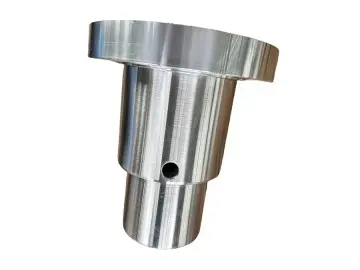
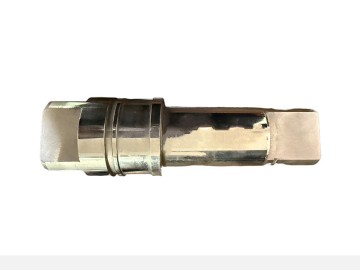
Explore our precision-machined blowout-proof valve stems, shafts, and gland configurations engineered to elevate safety standards across high-demand residential water and gas networks.
In contemporary plumbing systems, fluid delivery demands have dramatically intensified. The proliferation of multi-story domestic architectures, smart residential heating networks, multi-zone hydronic boilers, and city gas integrations has placed unprecedented operational stress on valve components. Historically, severe valve failure in domestic contexts was dominated by joint corrosion or seal degradation. However, under high hydraulic pressure surges, severe thermal expansion, and water hammer transients, the mechanical retention of valve stems has emerged as an indispensable safety frontier. Here enters the Anti-Blowout Stem for residential plumbing—a mechanical design milestone that precludes catastrophic stem ejection under peak pressurized dynamics.
Unlike top-loaded stem architectures vulnerable to retaining-nut failure, an anti-blowout stem is internally installed from the body cavity. A precision-forged integral shoulder seats securely against the valve internal shoulder, making axial blowout physically impossible even if external packing, glands, or handle retention clips are removed under full residential working line pressure.
Residential automated shutoff valves and fast-closing fixture solenoids routinely generate severe hydraulic shock waves (water hammer exceeding 300 psi). Our forged stainless steel stems absorb these extreme vertical shock loads effortlessly, ensuring flawless mechanical integrity and protecting occupants against catastrophic property flooding.
Manufactured using advanced grades such as 304, 316, 17-4PH, and specialized duplex alloys, these stems offer unmatched resistance to dezincification, pitting, and micro-crevice corrosion triggered by chlorinated city municipal water, chloramines, softened water chemistry, and elevated fluid temperatures.
The residential plumbing landscape is currently experiencing a profound paradigm shift driven by strict municipal codes, smart home IoT integration, and heightened environmental conservation. Where simple brass utility valves once sufficed, contemporary building regulations increasingly mandate fail-safe fluid control hardware. High-rise residential apartments utilize booster pump systems that maintain continuous high hydrostatic pressures. In these demanding environments, valve components equipped with anti-blowout stem architectures are recognized as an essential preventive risk mitigation standard.
Moreover, modern homeowners and utility managers prioritize long lifecycle valve infrastructure. Replacement of internal wall valves in residential structures incurs tremendous structural disruption and financial expense. By integrating internally seated anti-blowout stems forged from corrosion-resistant austenitic stainless steel, builders guarantee decades of smooth actuation, zero leakage paths, and impenetrable stem stability.
In tall residential complexes, static water pressure at lower levels must be strictly regulated yet can peak drastically during demand lulls. Main riser shut-off ball valves featuring anti-blowout stems withstand fluctuating differential pressures, ensuring maintenance technicians can service packing seals without risking hazardous stem dislodgement.
Closed-loop residential radiant floor heating and combi-boiler loops experience continuous thermal cycling between 20°C and 85°C. The integral shoulder design of the anti-blowout stem maintains uniform thrust-washer contact, preventing fluid bypass and handling aggressive glycol additives without structural fatigue.
Automated leak-detection motor actuators exert rapid torsional torque onto stem connections. Precision CNC-machined anti-blowout shafts paired with square couplings ensure zero rotational backlash and flawless sealing against residential natural gas or domestic water pipelines.
Standard commercial top-inserted valve stems rely entirely on an external gland nut, snap-ring, or bonnet thread to retain internal pipeline pressures. Under prolonged mechanical wear, overtightening, or thread stripping, such configurations are susceptible to sudden explosive ejection. Conversely, our Anti-Blowout Stem design leverages fluid dynamics to enhance safety: internal line pressure naturally forces the stem's integral bottom shoulder firmly upward against the valve body seating collar, thereby strengthening the seal as line pressure rises.
Combined with PTFE, RPTFE, or PEEK low-friction thrust bearings, the anti-blowout assembly minimizes operating torque while completely eliminating galling between metal surfaces during frequent shutoff cycles. This dual advantage guarantees whisper-quiet operation in smart domestic plumbing automation setups.
Sichuan Yining Machinery Equipment Co., Ltd. was established in 2005 and is a company specializing in the production and manufacturing of various types of valves and finished valve accessories. Over the years, we have been dedicated to the field of valves and are committed to providing high-quality and high-performance products and solutions to customers worldwide.
The company has always adhered to the business philosophy that "Quality is the boss, quality is our salary", insisting on taking quality as the core and regarding stable and reliable product quality as the solid foundation for long-term cooperation with customers. We are well aware that high-quality products and stable delivery capabilities are the keys to the continuous development of an enterprise.
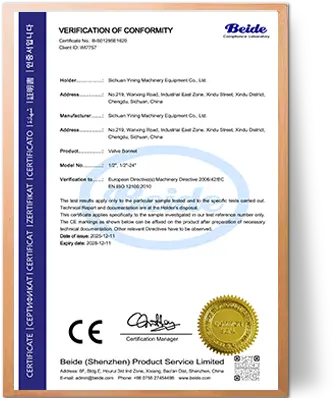
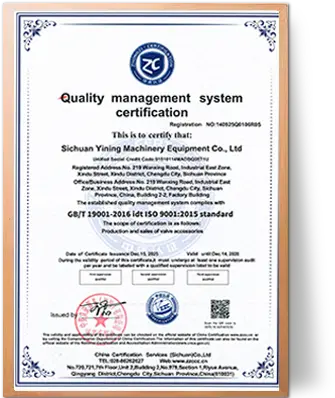
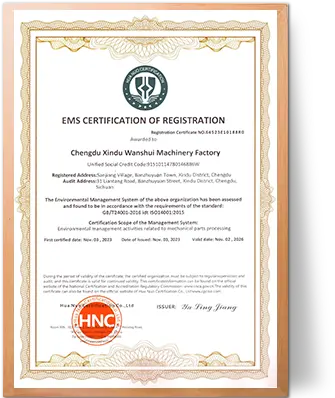
The company has passed the ISO9001 quality management system certification and CE certification, and strictly follows international standards for production and quality control to ensure that every product meets industry and customer requirements.
With years of manufacturing experience and mature production techniques, we have a professional technical and management team with rich theoretical knowledge and practical experience. We adhere to the development direction of "conceptual innovation, technological innovation, and management innovation", constantly improving product quality and enterprise competitiveness.
In the future, Sichuan Yining Machinery Equipment Co., Ltd. will continue to take outstanding quality as the core, customer demands as the orientation, and join hands with partners to create a long-term, stable and mutually beneficial win-win cooperative relationship.
 +86-15208308717
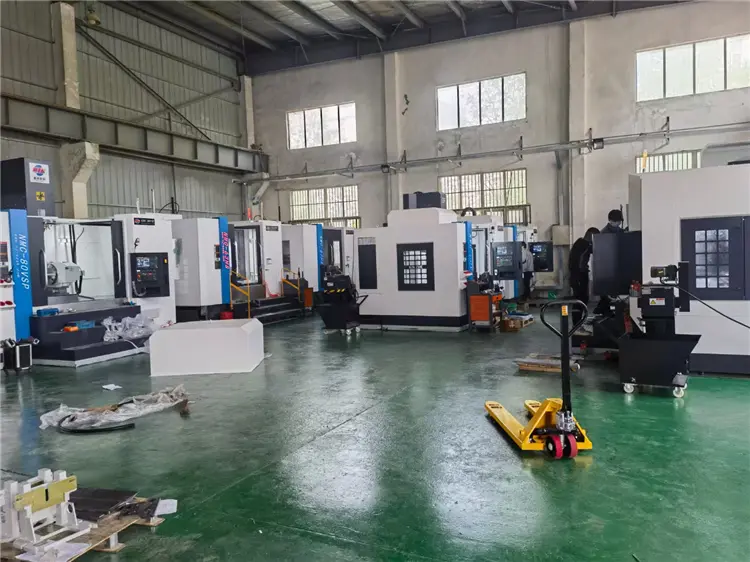
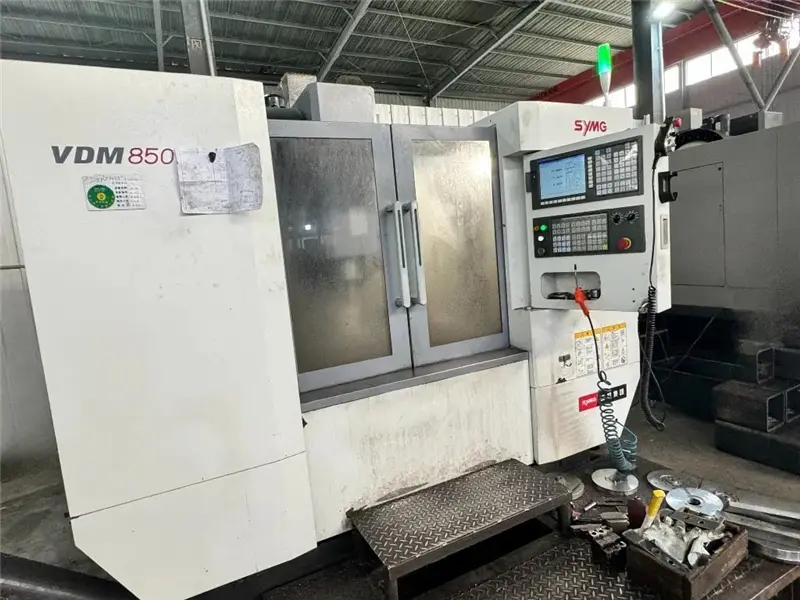
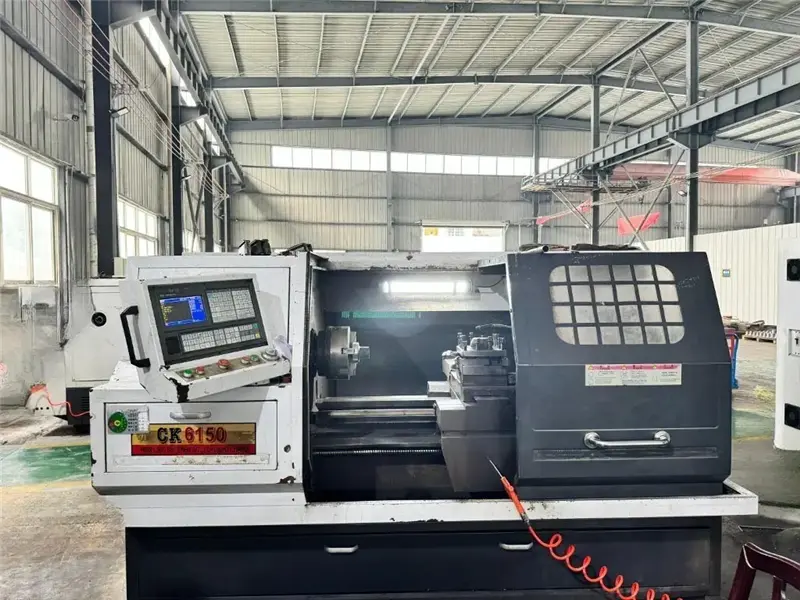
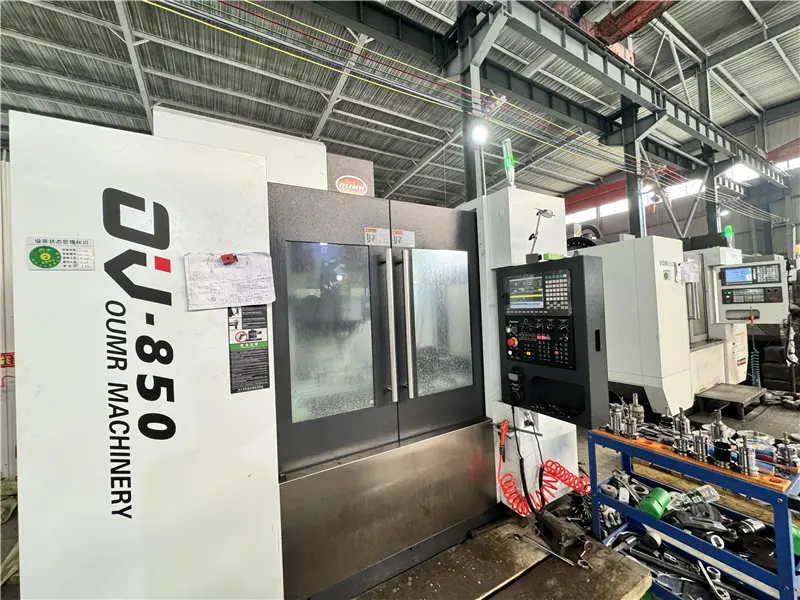
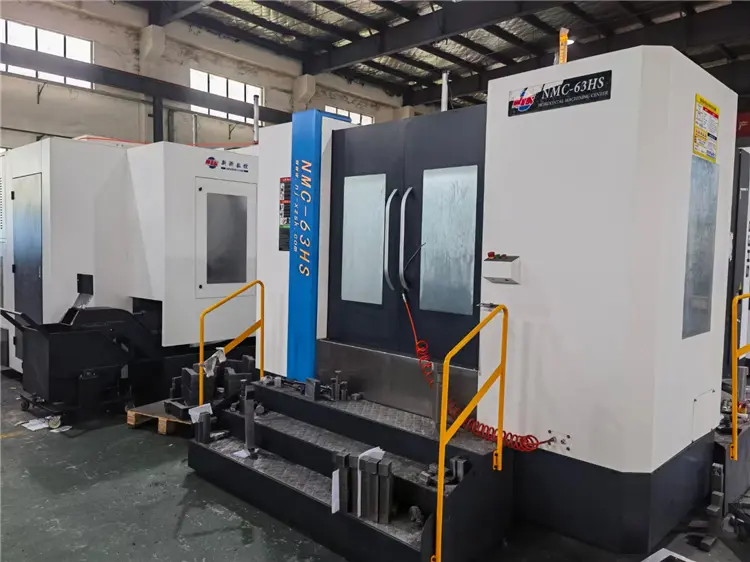
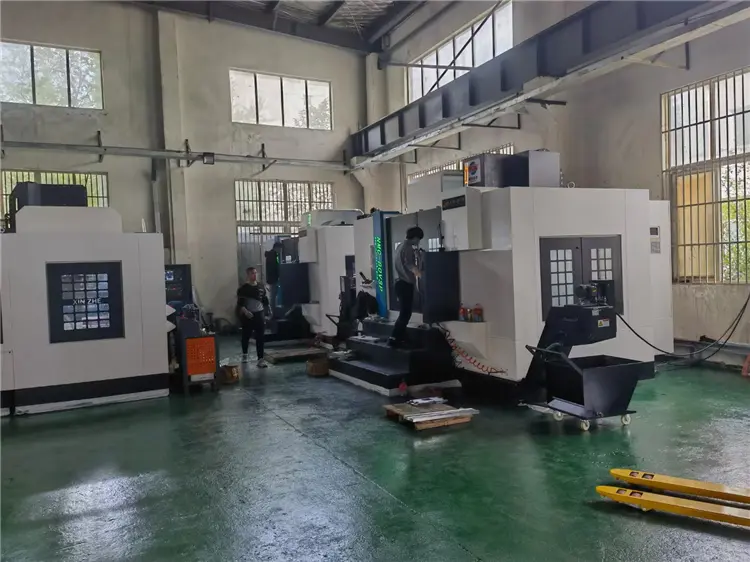
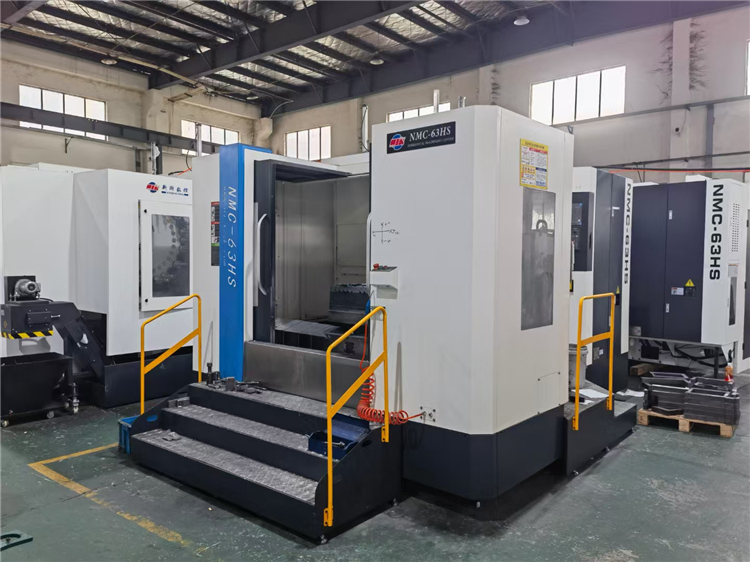
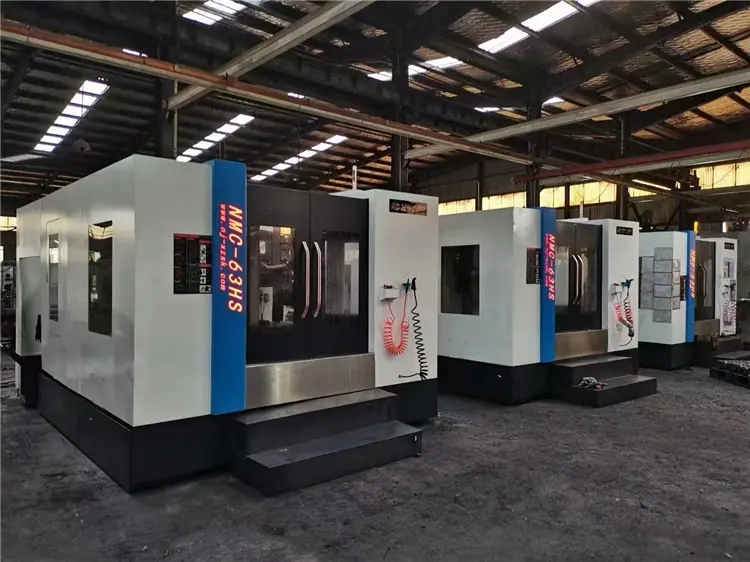
Our company is CE certified and operates under an ISO 9001 quality management system. We are equipped with CNC machines, machining centers, forging and cold forming equipment, as well as physical and chemical testing facilities.
Our valve components are manufactured in accordance with GB, ANSI, JIS, DIN, and BS standards, meeting the conformity requirements of international markets, including Europe.
We machine carbon steel, stainless steel, alloy steel, and special materials such as 410, 420, F304, F316, LF2, A105, 17-4PH, Monel 400, and XM-19, and support custom production based on customer drawings.

In addition to comprehensive product supply, our service level is also outstanding. With rich experience in the industry, we are always able to deeply understand the needs of our customers and meet all kinds of OEM customisation requirements. We ensure on-time delivery, prompt response and take care of all after-sales issues.
Sichuan Yining Machinery Equipment Co., Ltd. is committed to becoming a trusted partner of global valve companies.
Explore Packing Gland Assemblies & Stem Sealing StructuresTake an inside look at our advanced CNC machining workshops, forging plants, and testing grounds where our anti-blowout valve stems and residential plumbing solutions are precisely crafted.